中国专业光学镜片模具及光学组件及光学成型及光学镀膜供应商
先进光学能力


Optical Lens Tolerances: What to Specify on an RFQ
9 月 15, 2026
An optical lens RFQ is easier to quote and manufacture when the drawing separates performance-critical requirements from general preferences. Overly broad or unnecessarily tight tolerances can increase tooling, inspection and production cost without improving the final system.
The goal is to define what the assembled optical system needs and give the supplier a clear method for verifying it.
Separate Optical Performance From Mechanical Fit
Begin with the optical function: focal length, optical power, wavelength range, image quality, beam shape or illumination distribution. Then define the mechanical interfaces that locate the lens in the assembly. This separation helps the supplier identify which dimensions control optical performance and which dimensions control fit.
Key Optical Tolerances to Review
Surface form and irregularity
Surface form describes how closely the manufactured surface follows the nominal design. The appropriate specification depends on the lens type, aperture, wavelength and system sensitivity. State the measurement method and clear aperture so results can be compared consistently.
Surface quality
Scratch-dig or an equivalent cosmetic standard should be connected to the functional area. A viewing window, imaging lens and hidden illumination optic may require different acceptance criteria. Mark cosmetic zones where appearance matters.
Centration and decenter
Optical axis alignment can be expressed through centration, wedge, runout or decenter controls. The drawing should make the datum structure clear and show how the lens is located during assembly and inspection.
Thickness, diameter and edge geometry
Center thickness, outside diameter, flange dimensions, edge thickness and mounting features affect both optical spacing and mechanical assembly. Avoid placing tight tolerances on every dimension. Identify the features that establish position and allow reasonable clearance elsewhere.
Coating Requirements Need More Than a Name
“AR coating” is incomplete without a wavelength range, angle of incidence, polarization condition and performance target. Include environmental exposure, adhesion expectations and cosmetic criteria. For coated plastic optics, the substrate temperature limit and surface preparation also need consideration. See the optical coating capability page for related planning points.
Define Inspection and Sampling
- Identify the applicable drawing standard and units.
- State the clear aperture and excluded edge zones.
- Define the test wavelength and measurement condition.
- List any required reports, samples or retained records.
- Clarify whether inspection is 100% or based on an agreed sampling plan.
For molded optics, agree how tool qualification, first articles and production monitoring will be handled. A measurement that works for a few prototypes may be too slow or unstable for routine production.
A Practical Optical Lens RFQ Package
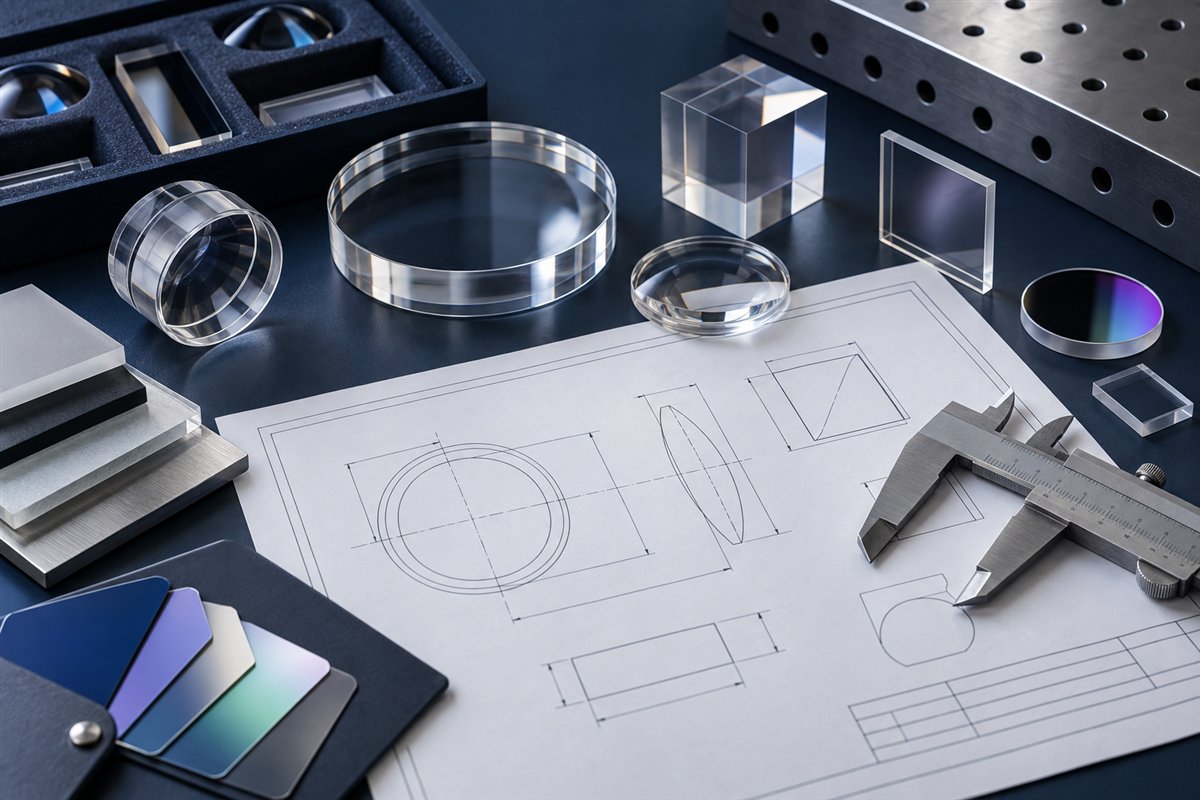
Include a 3D model, controlled drawing, optical prescription or performance target, material requirement, coating specification, expected quantity, annual demand, assembly context and operating environment. Mention the intended development stage: feasibility, prototype, pilot or released production.
If some tolerances are still open, label them for supplier review. That invites a useful DFM response and prevents assumptions from becoming hidden cost.
Frequently Asked Questions
Should every optical tolerance be as tight as possible?
编号. The most economical specification controls the characteristics that affect system performance while allowing practical manufacturing variation elsewhere.
Can a supplier quote from a 3D model alone?
A model can support an early estimate, but a production quote normally needs material, optical, cosmetic, inspection and quantity requirements.
When should tolerances be reviewed?
Review them before tool release and again after prototype or first-article testing, when system-level evidence is available.
For a drawing review, use the Silver Optics contact form and include your target application, files and expected volume.
也许你也喜欢
服务 & 产能
资源
获取免费报价
复制©2025 | 银光学. | 版权所有
服务
